A multi-layer insulator comes off a thermal cutter with a fused edge where heat reached the adhesive layer. A heat shield print calls out full material properties at the cut edge, and half the quotes cannot meet it. A prototype needs a revised contour by Friday, and one shop quotes a program change while another quotes new tooling.
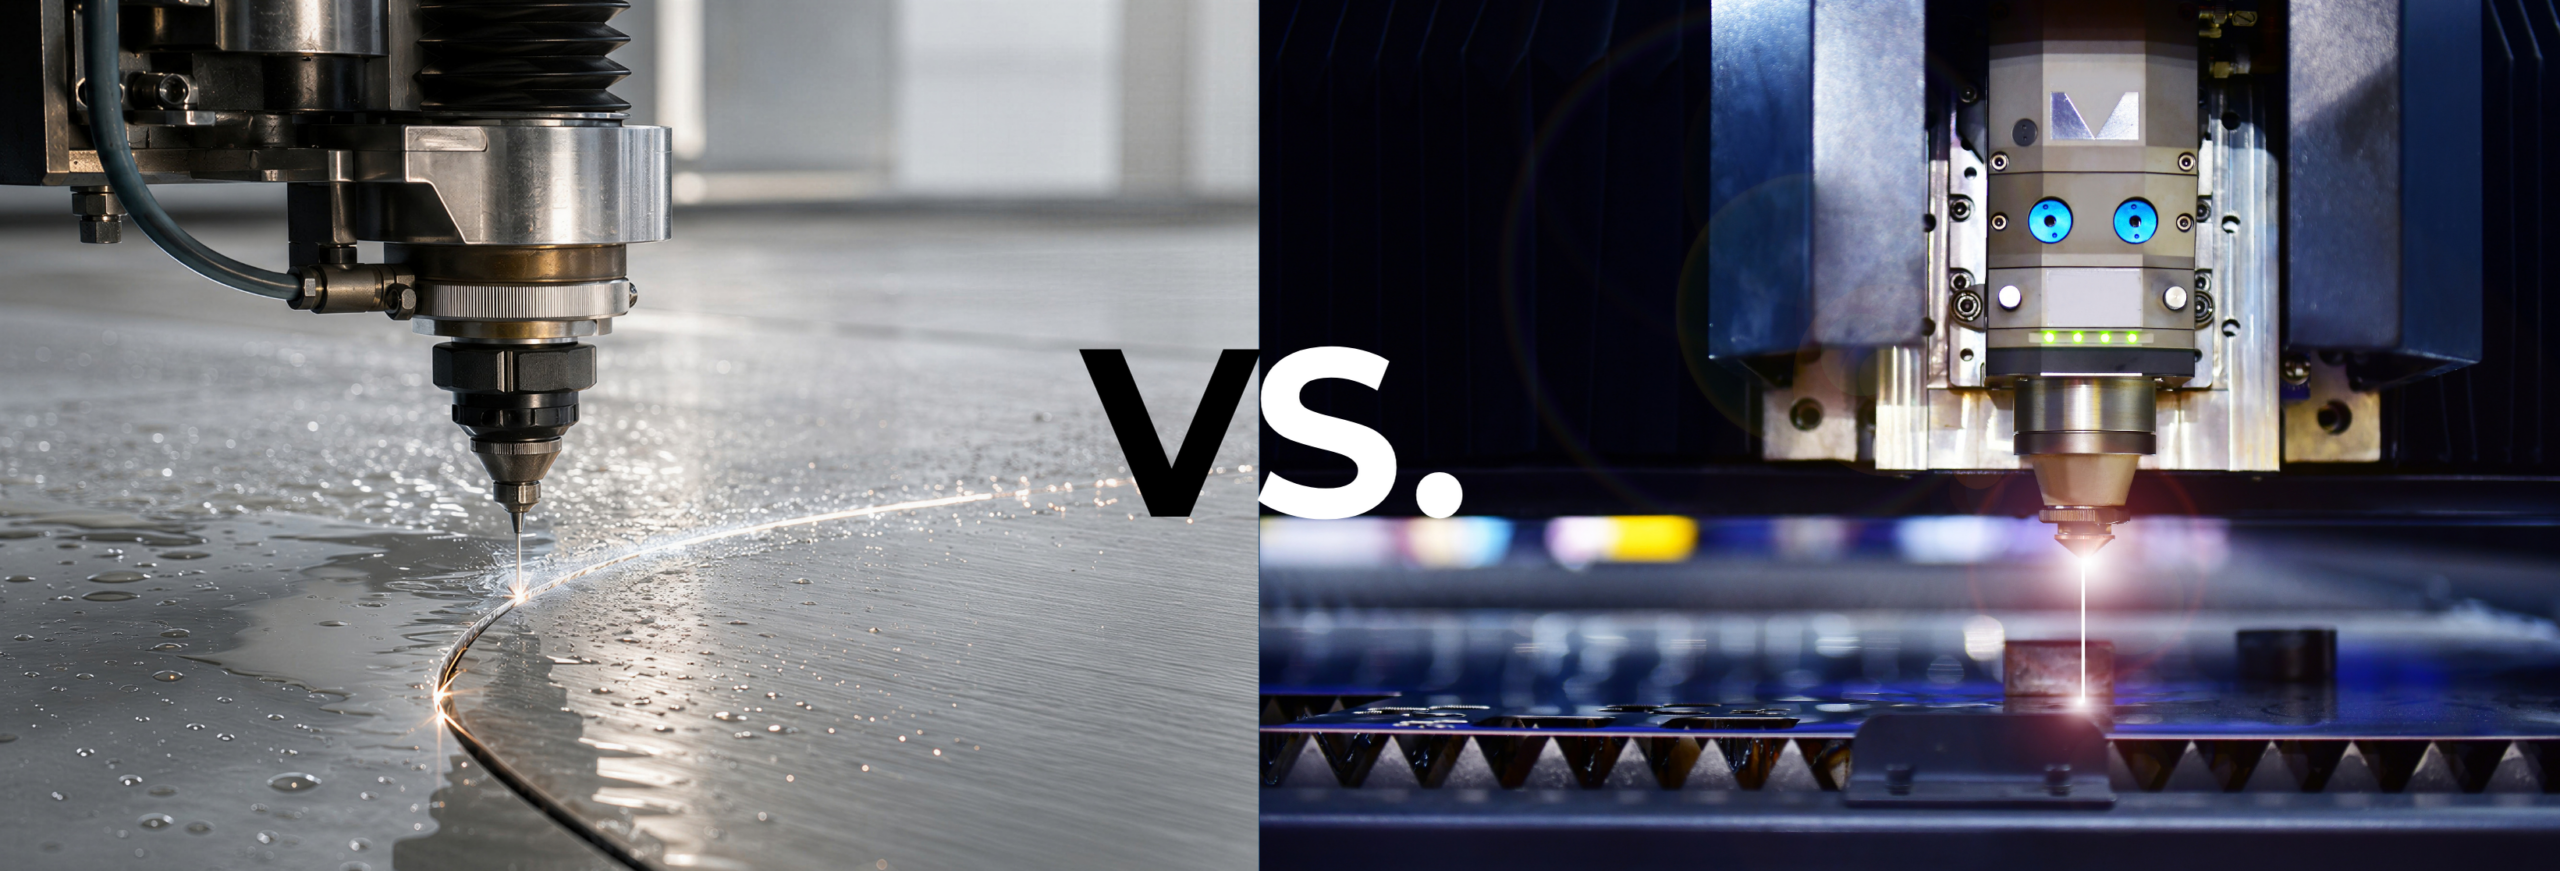
Sourcing teams see all three situations, and each one traces back to the same early decision: which cutting process the part was built around. Water jet cutting and laser cutting both turn material into finished geometry, and they do it in ways different enough that the wrong choice shows up later as scrap, rework, or a missed launch date.
This guide compares water jet cutting vs laser cutting for OEM production: how each process works, where each one wins, and how to match the method to the part in front of you. By the end, you will know what each process does to your material, what accuracy to expect from each, and which questions settle the choice before tooling money gets spent.
How Water Jet Cutting Works
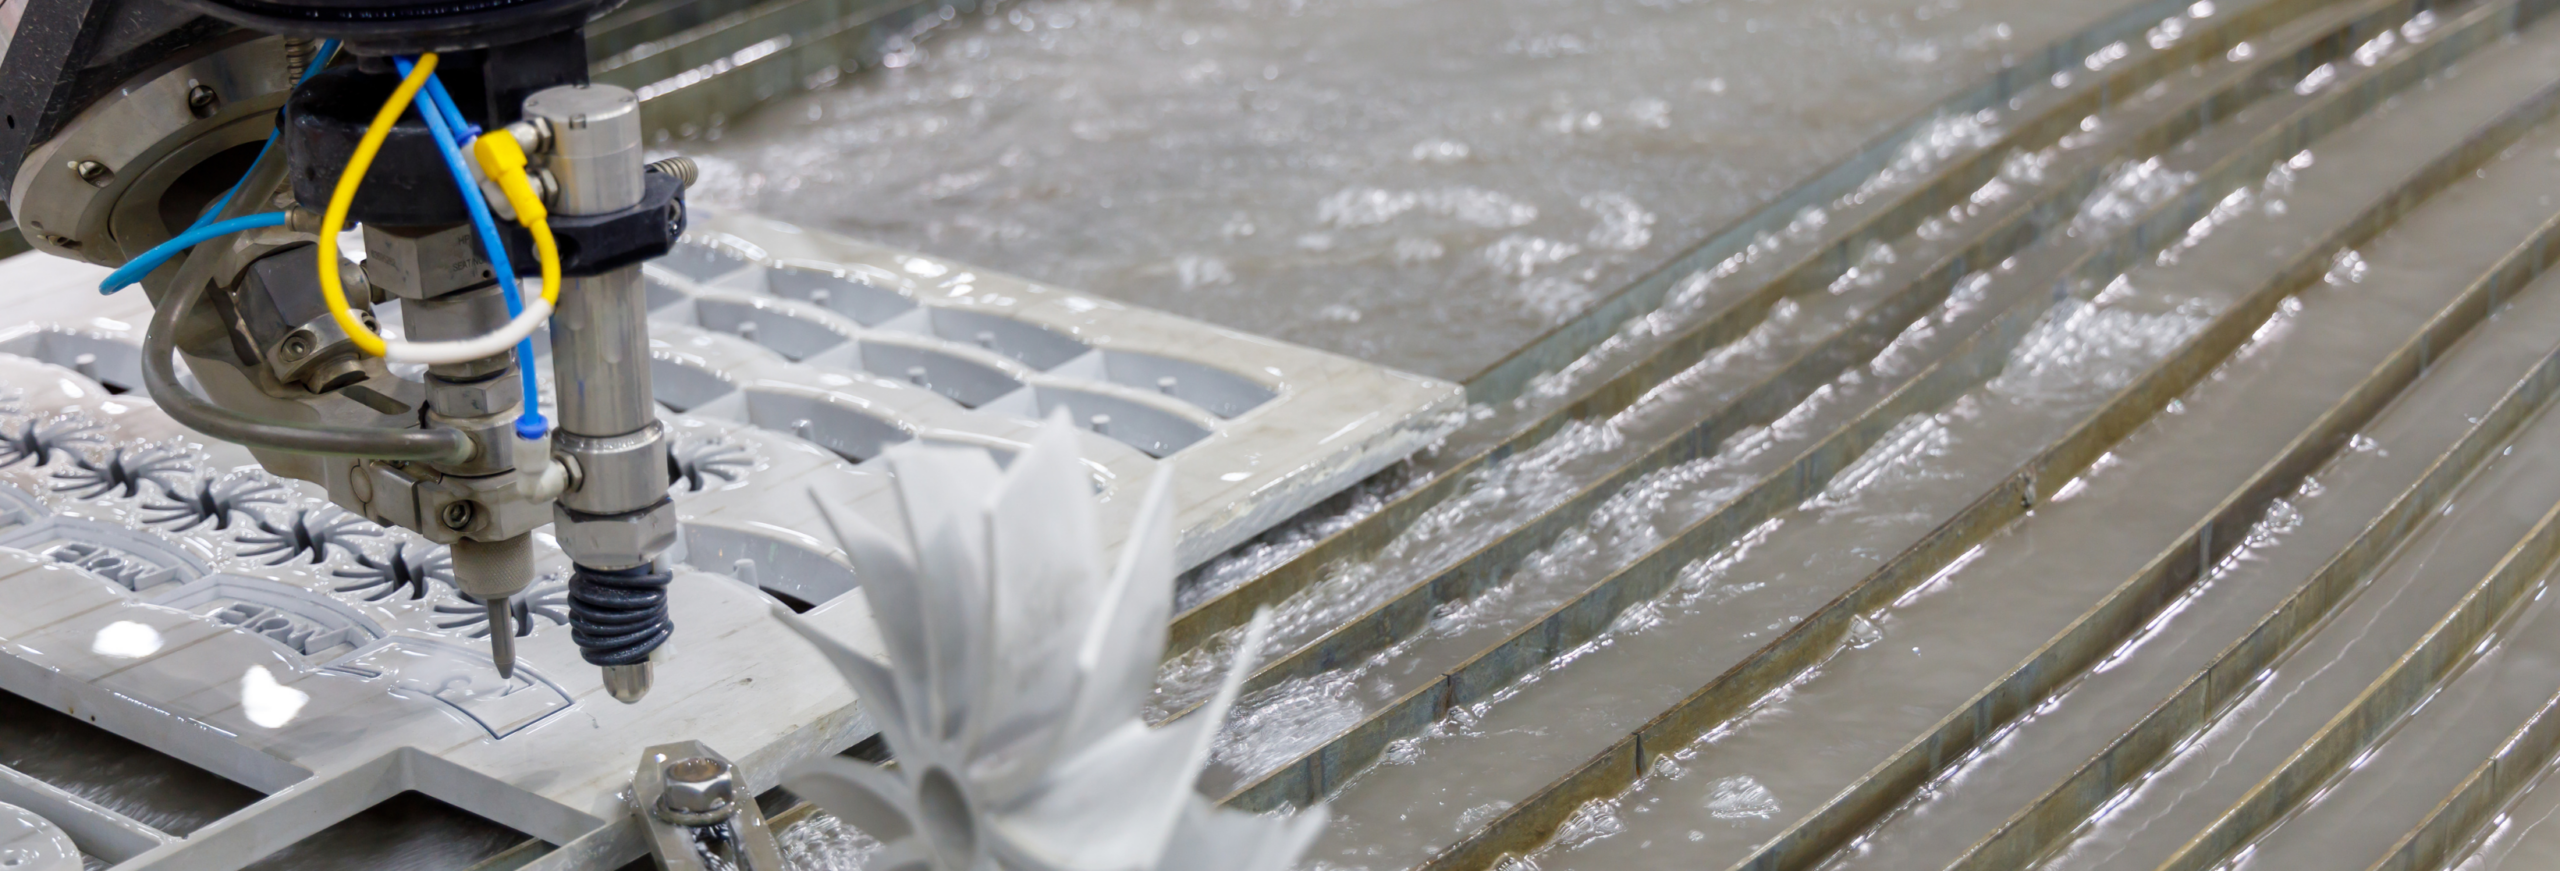
A waterjet system pressurizes water and releases it through a small orifice cut into diamond or sapphire. According to ESAB, typical cutting pressure runs between 50,000 and 60,000 PSI, with newer systems reaching 90,000 PSI, released through an orifice between 5 and 15 thousandths of an inch in diameter. For soft materials such as foam and rubber, the water alone does the cutting. For harder materials, garnet abrasive mixes into the stream inside the cutting head, and the abrasive does the work.
The sequence looks like this:
- A pump pressurizes water to ultra high pressure.
- The water releases through the orifice, forming a thin, supersonic stream.
- For hard or dense materials, abrasive feeds into the stream in a mixing chamber.
- The stream erodes material along the programmed path, and the spent water and abrasive collect in a tank below the part.
The process works like sawing, not burning. Because no heat enters the material, the part comes off the machine in the same condition it went on. Edges stay clean, adhesive layers stay bonded, and heat treated or temper sensitive materials keep their properties through the cut. That single trait drives most of the waterjet cutting benefits that matter to OEM buyers.
How Laser Cutting Works
A laser cutter focuses a high energy beam of light to a point small enough to melt or vaporize material along the cut path. An assist gas, typically nitrogen or oxygen, blows the molten material out of the cut. The machine moves the cutting head across the sheet following the programmed geometry, the same way a waterjet does.
On thin, single layer sheet metal, laser cutting is fast, precise, and inexpensive per part. The beam produces a narrow kerf, holds fine detail, and runs at speeds a waterjet cannot match on the same stock. The tradeoff arrives as heat. The beam creates a heat affected zone along the cut edge, a band of material where the thermal input has changed the microstructure. According to Fathom Manufacturing, that zone can cause brittleness, oxidation, or corrosion along the edge and may require secondary operations such as deburring or finishing to correct.
The severity depends on the material. Aluminum and high strength steels lose strength in the area around a laser cut because the heat undoes local tempering. Reflective metals complicate the process further, because the surface bounces the beam instead of absorbing it. And on laminated or bonded materials, the heat that cuts the top layer keeps traveling, which is why layered constructions and thermal cutting rarely mix. In aviation, where edge integrity is treated as flight critical, heat affected zones are a documented reason waterjet is preferred for many cut parts.
Where Each Process Wins
Set side by side, the two processes divide the work cleanly. The comparison below reflects typical production capability, with accuracy figures drawn from published fabrication sources.
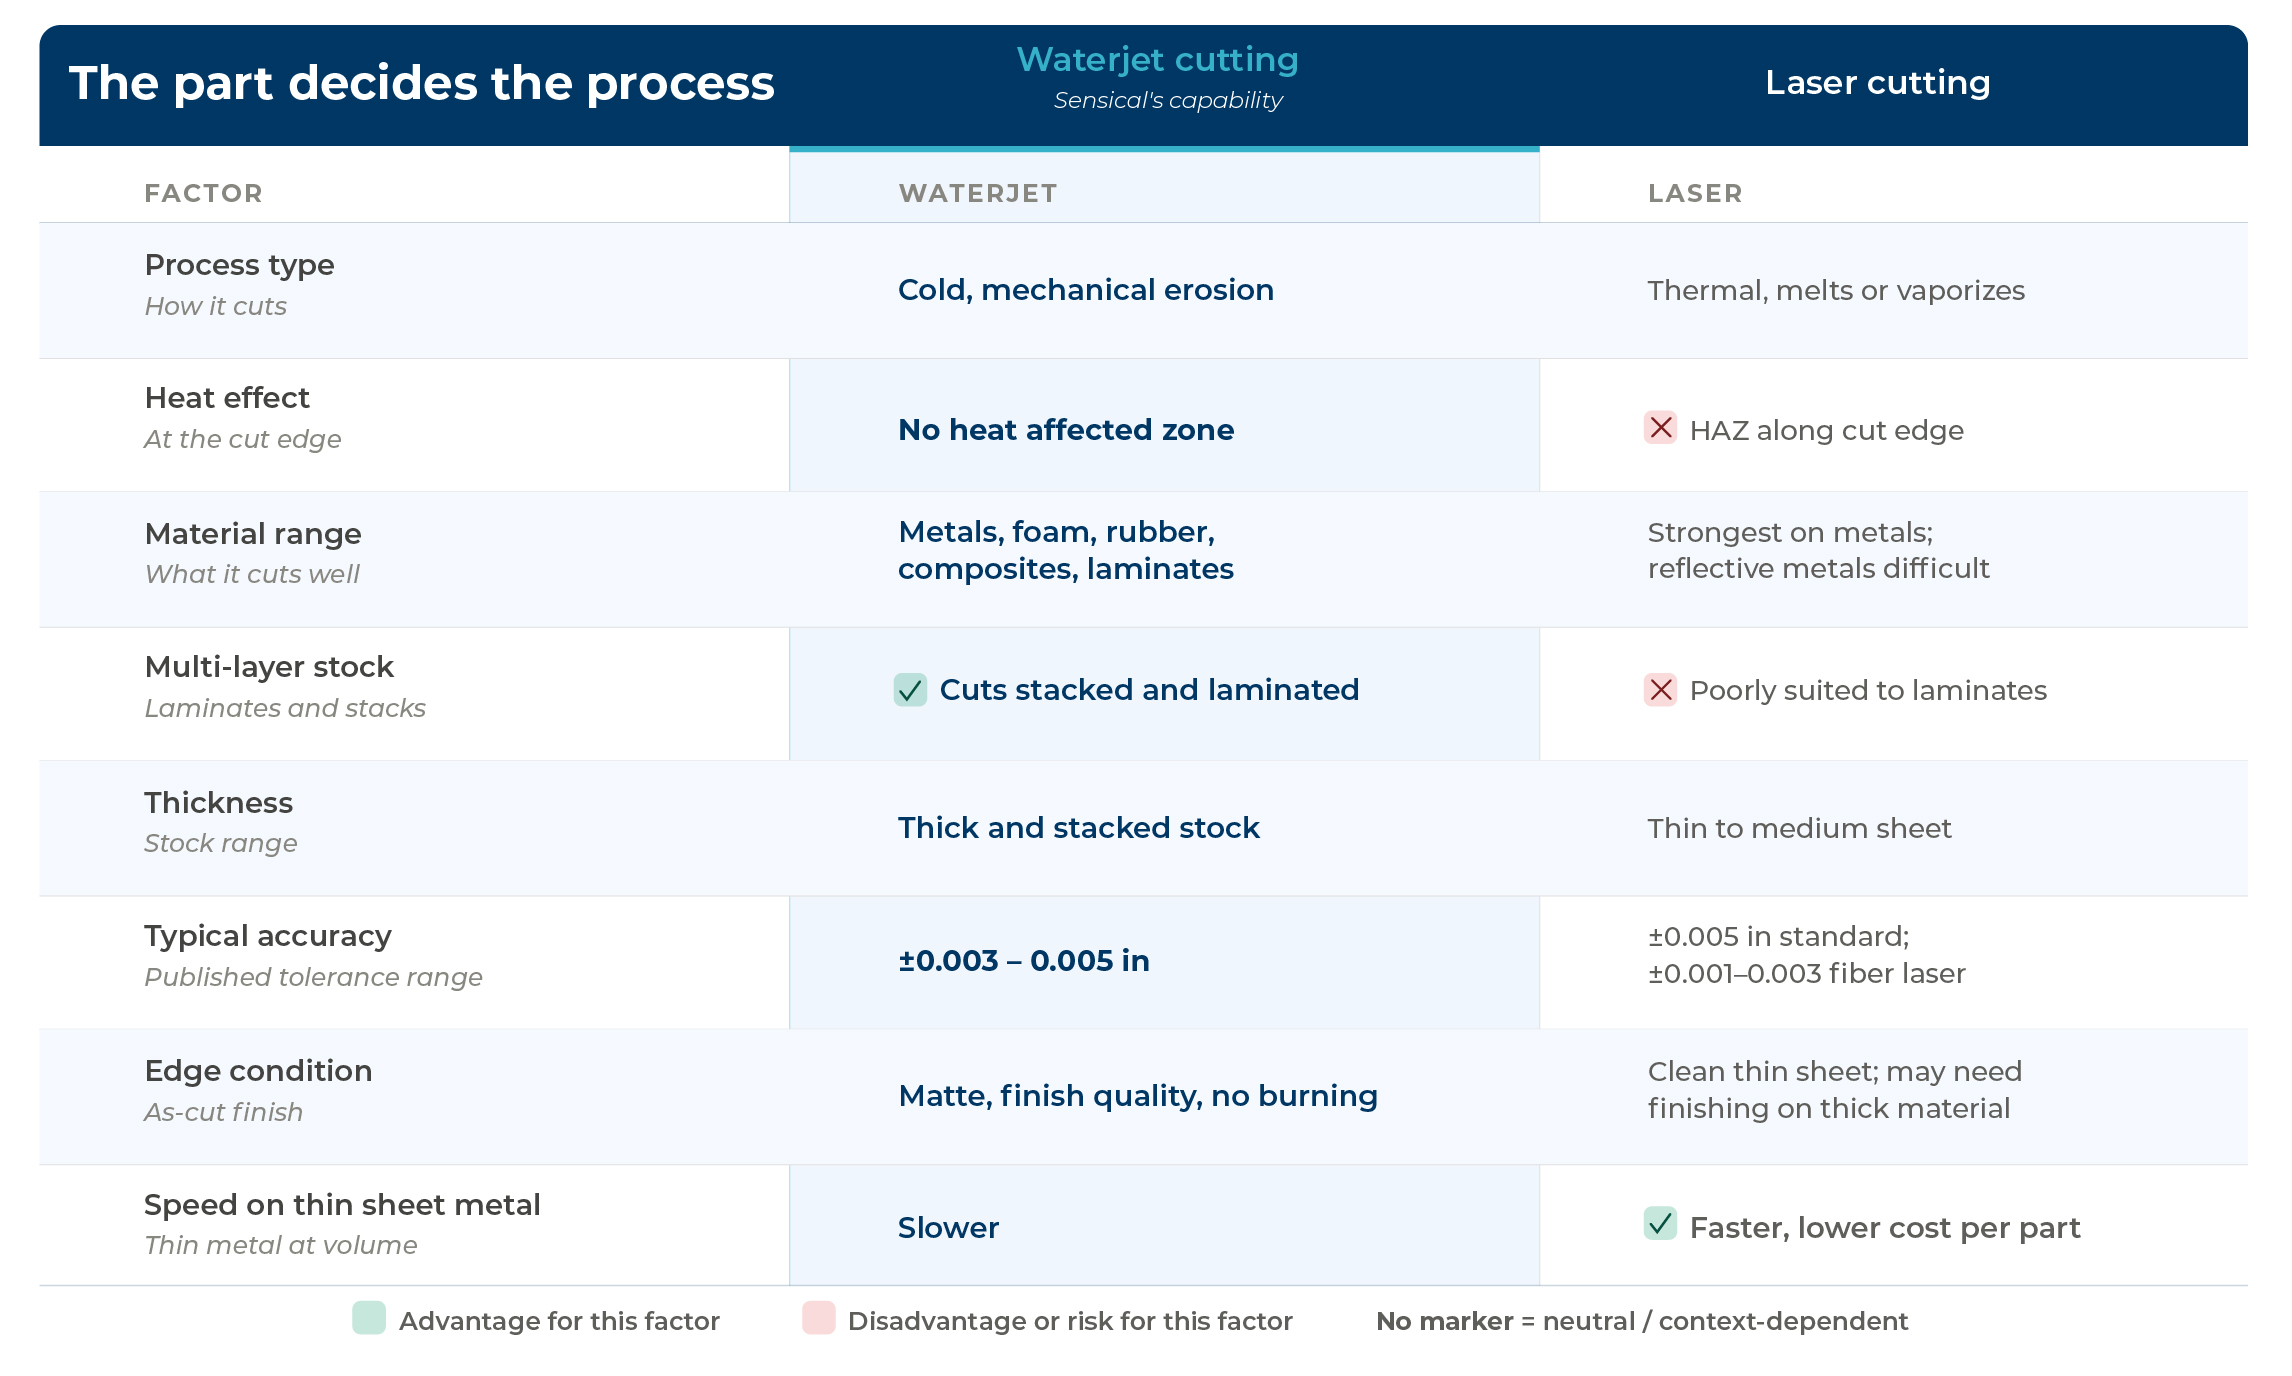
The part decides the process. Thin, single layer metal with fine detail at volume points to laser. Layered constructions, formed parts, heat sensitive alloys, and thick or mixed materials point to waterjet. A shop that runs only one of the two will tend to quote the process it owns, which is worth remembering when the recommendations start arriving.
Laser Cutting vs Waterjet in Automotive Manufacturing
Automotive work puts the difference between the two processes under real pressure, because so many automotive parts combine materials rather than using one.
Consider the acoustic and thermal parts that fill a vehicle: dash insulators, hood insulators, tunnel insulators, undercovers, and heat shields. These parts pair fiber substrates such as glasswool and PET nonwoven with films, foils, and adhesives, and many of them come out of a compression mold as a formed, three dimensional shape that still needs its final trim. Cutting that trim with heat risks the layers. Cutting it with water does not.
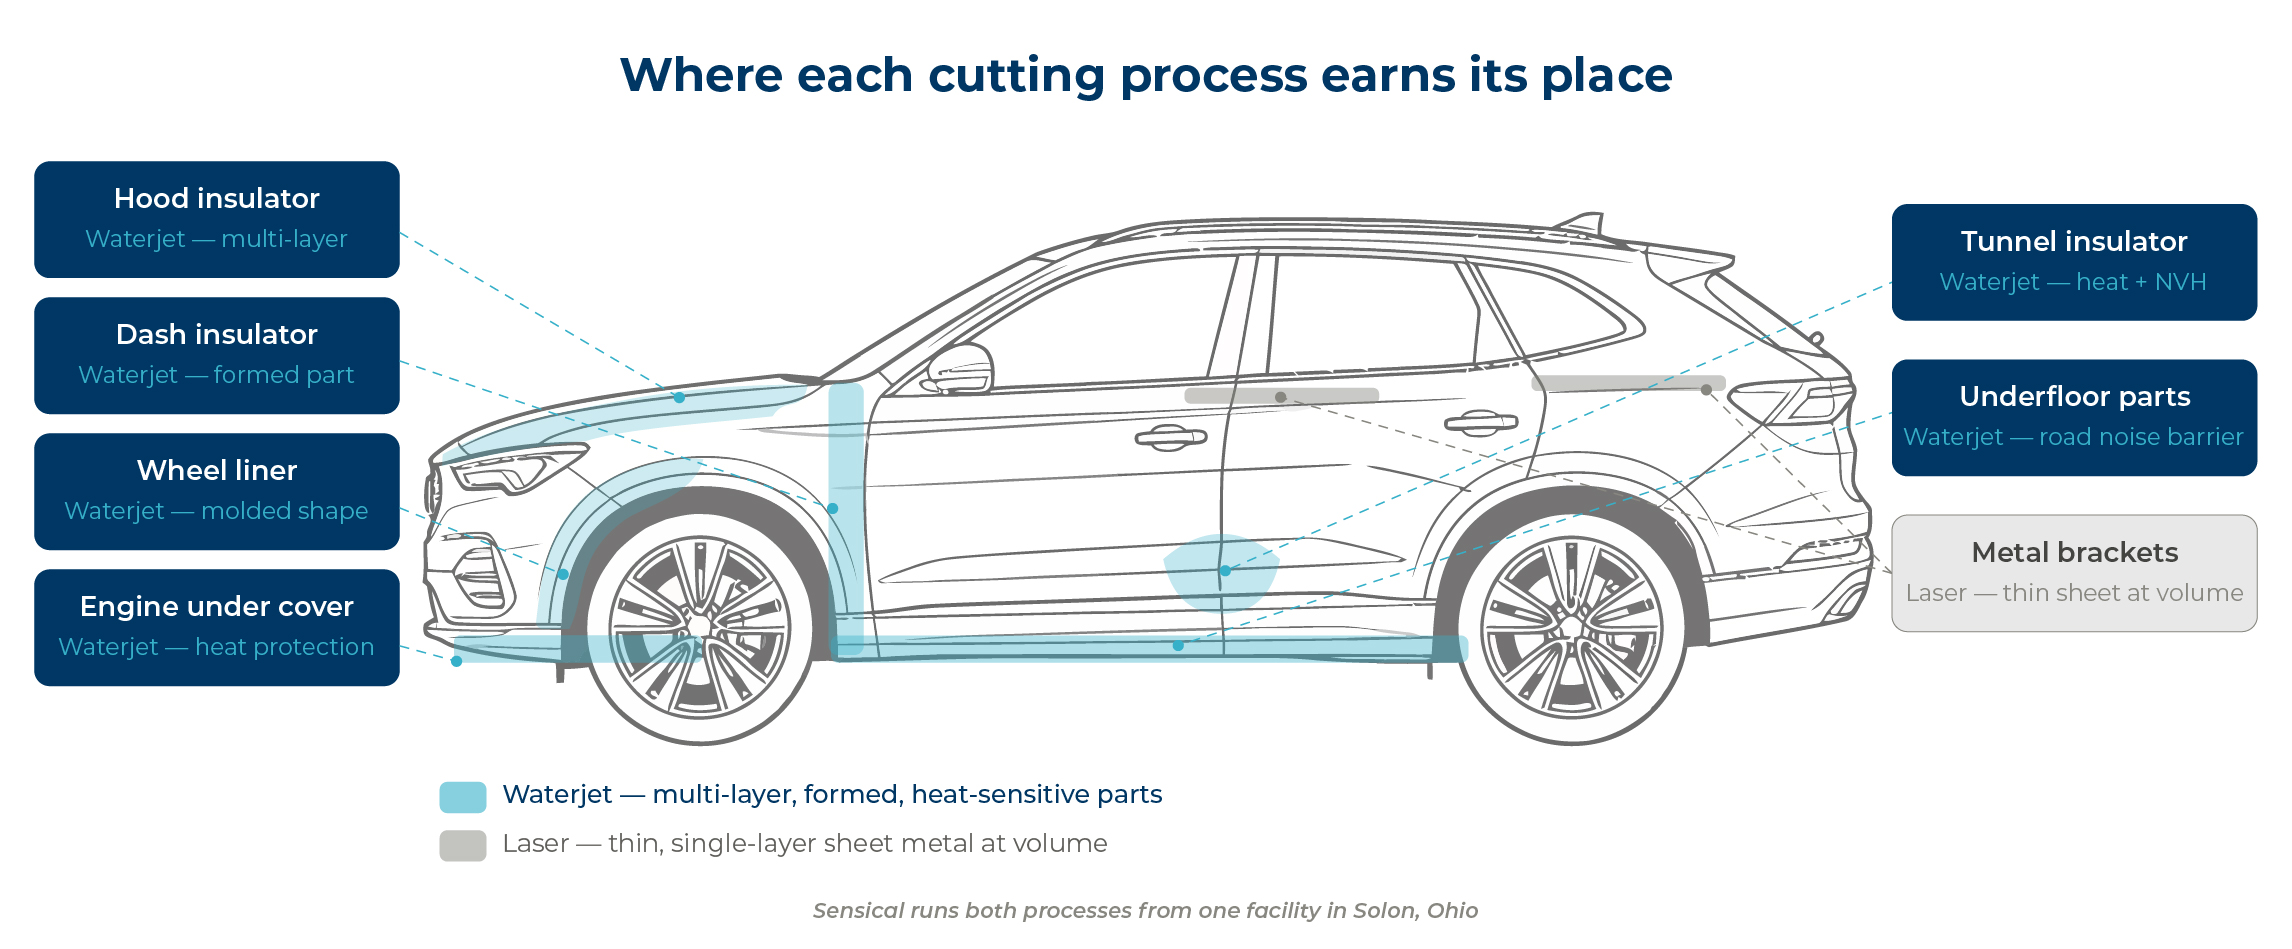
Where each process earns its place on automotive parts:
- Molded part post-trim. A formed insulator or heat shield needs its perimeter and openings cut after molding. Robotic waterjet systems follow the three dimensional contour and cut without adding heat to a part that just left a heated mold.
- Multi-layer materials. Laminated constructions, foil faced insulators, and adhesive backed assemblies cut clean under water. Thermal cutting risks fusing or delaminating the layers it touches.
- Aluminum heat shields. Aluminum reflects laser light and loses strength in a heat affected zone. Waterjet sidesteps both problems.
- Battery boxes and EV components. Battery enclosures pair formed geometry with barrier and seal materials, and they show up on waterjet part lists for the same reasons molded insulators do.
- Thin metal brackets and fine detail. Single layer sheet metal parts at production volume belong on a laser, where speed and per part cost win.
- Prototypes and soft, flexible materials. Laser cutting earns its keep on quick turn prototype work in softer flexible materials, where fine detail matters and heat risk is low.
Both processes share one economic advantage over die cutting: they cut from a digital file, with no hard tooling to build or modify. A revised contour becomes a program change instead of a new die, which is why both methods carry so much of the prototype and design revision work in a converting operation. The tooling savings compound on parts that change during development.
When automotive sourcing teams weigh laser cutting vs waterjet, the deciding question is usually what sits at the cut edge. A single material with no heat sensitivity gives you a free choice. Layers, adhesives, tempers, or a formed contour take the choice away.
Waterjet Cutting Accuracy for OEM Parts
Accuracy questions come up in every process conversation, and the honest answer is that both methods hold tolerances tighter than many converted and molded parts require. Published fabrication sources put waterjet cutting accuracy in the range of plus or minus 0.003 to 0.005 inches, with taper as the main watch item on very thick material. Laser cutting tolerance guides put standard laser accuracy at about plus or minus 0.005 inches on sheet metal, tightening to 0.001 to 0.003 inches on thin material with premium fiber machines.
For OEM parts, the more useful measure is repeatability at volume. A cutting process proves itself across a production run, not on a first article. Robotic waterjet systems hold part consistency across high volume runs because the program, the standoff, and the material indexing stay fixed, and because no thermal variable drifts as the machine heats up over a shift. On formed parts with three dimensional trim lines, robotic waterjet is often the only method that reaches the geometry at all.
Which Cutting Method for OEM Parts: How to Decide
The decision rarely needs a study. A handful of questions about the part settles which cutting method for OEM parts makes sense, and a capable supplier will walk through them with you before quoting.
Questions that settle the choice:
- What sits at the cut edge? Adhesive layers, laminations, tempers, and coatings argue for a cold cut. Bare single material leaves both options open.
- Is the part flat or formed? Flat sheet suits either process. A molded, three dimensional part that needs post-trim points to robotic waterjet.
- How thick is the stock? Thin sheet favors laser speed. Thick or stacked material favors waterjet.
- Does the spec call out edge condition or material properties? A print that requires full properties at the edge, or prohibits a heat affected zone, decides the question by itself.
- What is the volume? High volume thin metal rewards laser economics. Lower volumes and mixed materials narrow the gap or erase it.
A practical sequence for getting the method right:
- Send the full material specification, including every layer, adhesive, and coating, not just the base substrate.
- Call out edge condition and any heat restrictions on the print.
- State the volume and the launch timing, which drive the economics.
- Ask the supplier to recommend a process and explain the reasoning.
- Run a sample in the recommended process and inspect the edge before committing.
Sensical runs both processes, along with flatbed and rotary die cutting, from one facility in Solon, Ohio, so the recommendation follows the part rather than the equipment list. Robotic waterjet cutting post-trims compression molded parts every day, including aluminum heat shields, undercovers, tunnel insulators, and dash insulators in glasswool fiber and PET nonwoven, with multi-layer cutting and inline material indexing. Laser and die cutting run in the same building for the parts they serve better. The operation is ISO 9001:2015 certified, produces more than 90 million components a year for over 180 customers, and holds an average employee tenure of more than fourteen years, the kind of stability that shows up in the consistency of your parts.
Conclusion
The water jet cutting vs laser cutting question comes down to one physical difference: one process cuts with heat and one does not. Everything a buyer cares about follows from it. Laser wins on thin, single layer metal at volume. Waterjet wins wherever heat threatens the material, the layers, or the properties at the edge, and it reaches formed, three dimensional parts that a flat bed laser cannot.
The supplier worth a long term relationship is the one who runs more than one process, asks what sits at your cut edge, and recommends the method your part actually needs.
If you are weighing cutting methods for a part you are sourcing, start with a capability conversation. The right partner will ask as many questions as you do.
Frequently Asked Questions
What is the difference between water jet cutting and laser cutting?
Water jet cutting erodes material with an ultra high pressure stream of water and abrasive. It cuts cold, so the material keeps its properties and layered constructions stay intact. Laser cutting melts or vaporizes material with a focused beam of light. It cuts faster on thin sheet metal but creates a heat affected zone along the edge that can change material properties.
What are the benefits of waterjet cutting?
The main waterjet cutting benefits are the absence of a heat affected zone, a material range that covers metals, foams, rubber, composites, and laminates, the ability to cut thick and multi-layer stock, a finish quality edge that often needs no secondary work, and the reach of robotic systems on formed, three dimensional parts.
Is waterjet or laser cutting more accurate?
Both hold tight tolerances. Published fabrication sources put waterjet accuracy around plus or minus 0.003 to 0.005 inches and standard laser accuracy around plus or minus 0.005 inches, with premium fiber lasers reaching 0.001 to 0.003 inches on thin sheet. Thickness loosens tolerance for both processes. For most OEM parts, repeatability across a production run matters more than the first article number.
When should automotive OEMs choose waterjet over laser?
Choose waterjet when the part is laminated or multi-layer, when the material is heat sensitive or loses strength in a heat affected zone, when the part is a formed three dimensional shape that needs post-trim after molding, or when the print calls out full material properties at the cut edge. Choose laser for thin, single layer sheet metal with fine detail at production volume.
Does Sensical offer water jet cutting in Ohio?
Yes. Sensical runs robotic waterjet cutting from its facility in Solon, Ohio, post-trimming compression molded automotive parts and cutting multi-layer materials, alongside laser cutting and die cutting in the same building. The operation is ISO 9001:2015 certified and serves OEMs across automotive, appliance, and industrial markets.